Critical Inspection Points for Optimal Performance
Thus, a sleeve stabilizer is preserved by the detection of wear or damage before to returning the tool to service. It is necessary to inspect the whole assembly, not just the exposed surface of the sleeve.
Visual Examination
Start with a clean stabilizer and examine the mandrel and sleeve under adequate lighting.
Check for:
- Cracks, visible deformation, or abnormal surface damage
- Excessive wear on the sleeve OD
- Missing, chipped, or badly damaged hardfacing
- Localized wear or unusual contact marks
- Corrosion, pitting, or mechanical damage
- Damage around the sleeve seating and locking areas
- Damage to exposed connection surfaces
Record the location and type of any abnormal condition rather than simply marking the tool as “worn.” A consistent description makes it easier to compare the tool with previous run records and identify recurring problems.
If cracking, severe deformation, or other potentially critical damage is found, the tool should be evaluated under the applicable inspection procedure before being returned to service.
Dimensional Checks
Dimensional inspection is particularly important for a sleeve stabilizer because the sleeve provides the working OD that interacts with the wellbore.
Depending on the applicable drawing and inspection procedure, record relevant dimensions such as:
- Sleeve OD
- Mandrel dimensions
- Connection dimensions
- Overall length where applicable
- Any specified wear-related dimensions
Measurements must be made using calibrated equipment and compared to the appropriate drawings or acceptance requirements of the manufacturer.
Do not develop a general “maximum wear” value for all sleeve stabilizers. Acceptable limitations depend on the particular design and application. The Welong products are available in various sleeve sizes, hole-size combinations and connections, thus the relevant reference measurements should be determined by referring to the corresponding product specification.
Connection Integrity
Inspect all applicable rotary connections and connection surfaces for:
- Thread damage
- Galling
- Corrosion
- Deformation
- Damaged shoulders
- Foreign material or debris
- Evidence of abnormal make-up or breakout
If the sleeve assembly is changeable, examine the sleeve-to-mandrel interface and its locking or retention mechanisms according to the manufacturer's protocol.
Unless the corresponding manufacturer documentation specifies otherwise, do not use a general torque value, thread-locking compound, or retorquing interval. The method of construction varies with the specific sleeve stabilizer design.
API maintains standards and recommended practices for rotary drill stem elements . API Spec 7-1 API RP 7G-2 Inspection and Classification of Used Drill Stem Elements Inspection foundation should be determined using the appropriate edition and the operator’s inspection method.
Material Composition Analysis
Material checking is not a standard field maintenance procedure for each stabilizer. It is more applicable when there is a material identification issue, unexpected failure, suspected mix-up or demand from the operator’s quality system.
For particular applications refer to the specified material against the purchase documents and manufacturer's data. Welong Sleeve Stabilizers are offered in a variety of nonmagnetic, AISI 4145H and AISI 4145H MOD.
The test technique should be chosen according to the material and the aim of the study if a laboratory examination of the material is needed. It is not a replacement of the standard visual, dimensional and connection examination.
Troubleshooting Common Stabilizer Issues: Expert Tips
Relating the observed situation to probable causes and particular inspection locations makes troubleshooting more effective. Maintenance crews should also check the prior BHA setup and drilling data before modifying the stabilizer specification.
Uneven Wear Patterns
Uneven sleeve wear can indicate differences in BHA loading, contact conditions, alignment, formation behavior, or stabilizer configuration.
When uneven wear is found:
- Record the wear location and pattern
- Compare wear with the stabilizer's previous run records
- Review the stabilizer position within the BHA
- Check the sleeve dimensions and condition
- Inspect relevant BHA components for damage or abnormal wear
- Review drilling parameters and the formation interval where the wear occurred
Avoid assuming that uneven wear is caused by incorrect installation alone. The actual cause should be established from the available inspection and drilling data.
Premature Hardfacing Wear
Hardfacing wear should be evaluated together with formation abrasiveness, contact conditions, drilling parameters, and the selected hardfacing specification.
Check:
- The location and distribution of hardfacing loss
- Whether wear is uniform or localized
- The formation characteristics from the relevant hole section
- Previous run history
- The selected hardfacing specification
- Any changes in drilling parameters
Welong provides HF1000, HF2000, HF3000, HF4000 and HF5000 hardfacing choices for their Sleeve Stabilizer series. The largest number option is not always the best choice , you should choose the proper one according to the intended use .
Sleeve Loosening
Any evidence of sleeve movement should be treated as a condition requiring inspection before the tool is returned to service.
Check:
- The sleeve and mandrel interface
- Applicable locking or retention features
- Contact surfaces
- Evidence of abnormal movement or impact
- Damage that could affect the assembly
Avoid a standard retorquing or thread lock operation. Follow documented manufacturer’s installation and retention criteria for the specified sleeve stabilizer.
If no reason for movement can be found, the tool should be retained for additional investigation and not sent straight to the following run.
Magnetic Interference
For drilling programs that require non-magnetic equipment, the material and configuration of the stabilizer should be verified before the BHA is assembled.
Check:
- The purchase specification
- Material identification
- Stabilizer configuration
- BHA position
- MWD or directional-drilling requirements
- Any operator-specific magnetic-control procedure
For applications that need non-magnetic Sleeve Stabilizer arrangements, Welong is able to provide this.
Do not assume that it is the stabilizer which causes every magnetic anomaly. The full BHA and associated equipment should be tested in accordance with the operator’s directional and MWD protocols.
Extending Stabilizer Lifespan: Preventative Maintenance Strategies
A good preventive-maintenance program should integrate inspection, dimensional data, run history, and manufacturer requirements. The aim is not to extend the life of every instrument as long as feasible but to know when a component is still fit for purpose and when usage is no longer warranted.
Regular Cleaning and Inspection Protocols
After a run, clean the sleeve stabilizer sufficiently to expose the relevant surfaces for inspection.
Record:
- Visible damage
- Sleeve wear
- Hardfacing condition
- Connection condition
- Locking or retention condition
- Corrosion or pitting
- Relevant dimensional measurements
- Run information
Use the operator and manufacturer recommended cleaning and inspection techniques. Select the technique of NDT based on the material and suspected flaw where NDT is needed.
For surface breaking faults a suitable surface NDT technique should be used. Magnetic particle inspection is only applicable if the material and the process allow it. The inspection technique must be decided by the appropriate process and not chosen because it is usual practice in oilfield maintenance.
Precision Measurement and Tolerance Monitoring
Maintain dimensional records for each sleeve and, where applicable, the associated mandrel.
A useful record can include:
| Inspection Item | What to Record |
|---|---|
| Sleeve OD | Measured value and measurement location |
| Hardfacing | Wear condition and affected area |
| Mandrel | Visible damage and relevant dimensions |
| Connections | Thread and shoulder condition |
| Retention system | Condition and evidence of movement |
| Run history | Well, section, and relevant operating information |
Use the manufacturer's drawings and acceptance criteria when deciding whether a dimension remains serviceable. Do not apply a single generic wear limit to different sleeve sizes or designs.
This record also helps maintenance teams distinguish normal wear from recurring abnormal conditions.
Strategic Rotation and Inventory Management
A replaceable-sleeve system can make inventory planning different from that of a fixed-body stabilizer.
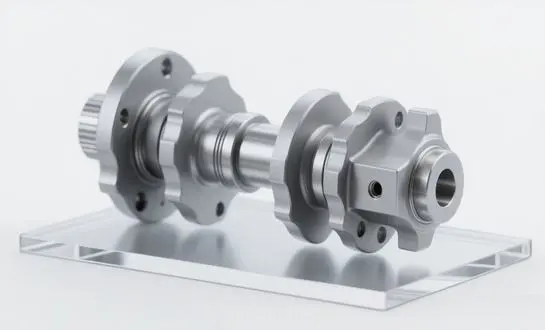
Welong's design uses an integral mandrel with interchangeable sleeves, allowing one mandrel series to accommodate different sleeve sizes.
For maintenance teams, this means inventory records can distinguish between:
- Mandrels
- Sleeves by size
- Hardfacing specification
- Connection configuration
- Service condition
- Inspection status
Instead of rotating tools simply to distribute wear, use actual run history and application requirements to decide which sleeve and mandrel combination should be deployed next.
Advanced Material Analysis and Upgrades
Material or hardfacing changes should be based on evidence from actual operating conditions.
Review:
- Repeated hardfacing wear
- Formation abrasiveness
- Sleeve wear rate
- Damage location
- Number of runs
- Maintenance findings
- Changes in drilling parameters
If the same wear pattern occurs, the data may be utilized as a reference for addressing an alternate hardfacing or material configuration with the manufacturer.
Welong offers a wide range of hardfacing and material configurations, such as AISI 4145H / 4145H MOD and non-magnetic choices.
Any enhancement suggested should still be validated against the BHA design and operational criteria and not assumed to be a general improvement.
Training and Skill Development
A maintenance checklist is only useful when the inspection team understands what each item is intended to identify.
Training should cover:
- Correct cleaning and inspection procedures
- Dimensional measurement
- Connection inspection
- Sleeve and mandrel identification
- Hardfacing assessment
- Documentation of wear patterns
- Applicable NDT procedures
- Manufacturer requirements
- Criteria for holding a tool for further evaluation
Inspection records should also be shared with drilling and engineering teams when recurring wear or damage is identified. This creates a feedback loop between field performance and future BHA selection.
A practical maintenance process can therefore follow:
Run → Clean → Inspect → Measure → Record → Evaluate → Service or Release
This is more useful than relying on a fixed calendar-based maintenance schedule without considering actual tool condition and run history.
Conclusion
A sleeve stabilizer should not be judged for wear by visual inspection alone. The mandrel, replaceable sleeve, hardfacing, size, connections and retention features must all be addressed before the tool may be restored to service.
The key premise is to isolate the observed state from the supposed reason. Uneven wear, loss of hardfacing, sleeve movement or dimensional changes should prompt a methodical examination and evaluation of the relevant BHA and drilling data. Do not use general torque values, maintenance intervals or wear thresholds, utilize manufacturer specifications for assembly requirements and serviceability constraints.
In systems using replacement sleeves, maintenance records may also help to improve inventory management by allowing the state of the sleeve and the condition of the mandrel to be recorded independently. Welong’s Sleeve Stabilizer provides a robust mandrel with a series of removable sleeves in various diameters, allowing drill teams to adapt to changing hole sizes or applications.
For more information about sleeve stabilizer specifications, replacement sleeves, material options, hardfacing, or application requirements, contact Welong at oiltools15@welongpost.com.